How to Choose the Right PCBA Manufacturing Partner?
Choosing a PCBA manufacturing partner can shape your product’s quality, launch date, and long-term reputation. The lowest quotation rarely tells the whole story. A reliable partner should explain its process clearly, from component sourcing and PCB assembly to inspection and shipment.
Look for practical evidence, not polished promises. Ask whether the factory uses SPI, AOI, and X-ray inspection where appropriate. Request sample inspection reports, traceability records, and documented corrective actions. A capable team should understand DFM reviews, component risks, soldering profiles, and IPC workmanship requirements. It should also explain how engineers handle prototype changes without creating confusion on the production line.
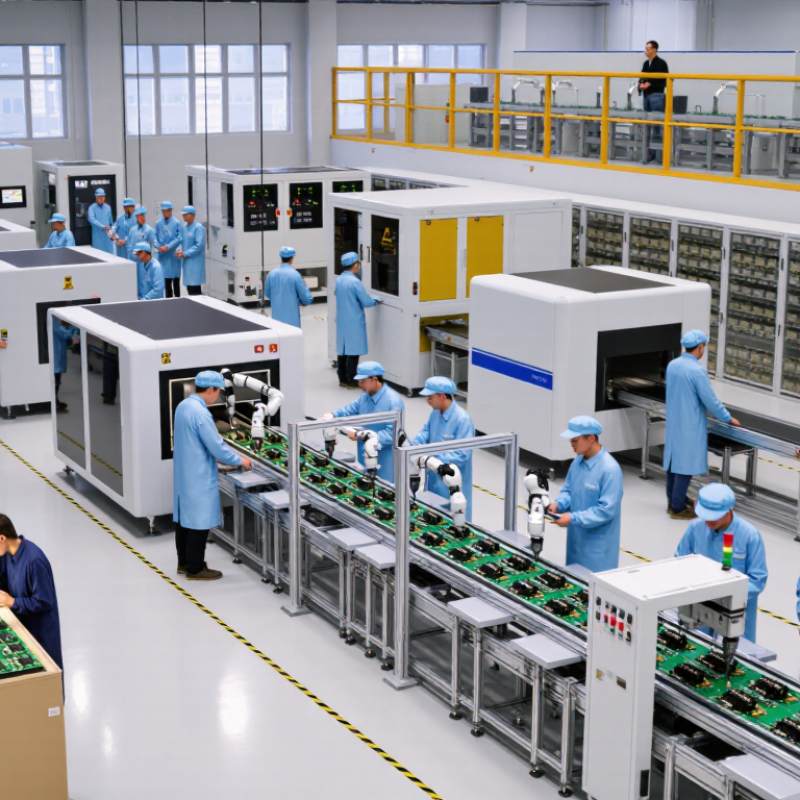
Factory experience matters. Visit the facility when possible. Watch how materials are labeled, stored, and moved. A clean line with visible process controls often reveals more than a sales presentation. Discuss production capacity, line flexibility, testing options, quality targets, and realistic lead times. The right partner should communicate early when a design, component, or schedule creates risk.
No supplier is flawless. Neither is every customer’s design. That reality deserves honest discussion. A partner that admits limitations may prove more dependable than one claiming perfect performance. Ask for references from similar products and industries. Check whether those customers received consistent support after delivery, not only during the first order.
Trust develops through measurable results. Select a PCBA manufacturing partner that combines technical discipline, transparent communication, and accountable service. Your decision should support today’s prototype and tomorrow’s scaled production. That balance is easy to overlook. It can become expensive later.
Defining Your PCBA Manufacturing Requirements
Defining PCBA manufacturing requirements starts before requesting a quotation. A purchasing brief should state board dimensions, layer count, materials, copper weights, and expected annual volume. Include component package types, smallest pitch, placement tolerances, and whether through-hole assembly is required. Be specific. I have seen projects slow down because “high quality” replaced measurable acceptance criteria. That phrase sounds reassuring, but it is difficult to audit.
Describe electrical testing, visual inspection, programming, traceability, and record retention needs. Specify test coverage and acceptable defect limits. If the board supports medical, automotive, or industrial equipment, identify applicable regulations and documentation requirements. Ask the manufacturer to explain process controls, equipment calibration, defect handling, and engineering change approval. Their answers should include evidence, not polished promises. Site audits and sample reviews can reveal gaps that documents hide.
Build a realistic timeline for prototypes, pilot runs, and regular production. State forecast changes, approved component alternatives, packaging requirements, and shipping conditions. A capable partner should identify missing data and challenge risky assumptions before quoting. I have also learned that my own forecast was too optimistic. A flexible capacity plan prevented a painful delay. Leave room for review. Requirements evolve.
Reviewing Quality Systems, Certifications, and Testing Methods
How to Choose the Right PCBA Manufacturing Partner?
A reliable PCBA partner proves quality through controlled systems, not attractive promises. Review ISO 9001 certification, audit dates, scope, and corrective-action records. Automotive projects may require IATF 16949. Medical assemblies often need ISO 13485 controls. Certification alone is not enough. A supplier can pass an audit and still miss a weak via.
Ask how operators control solder paste, humidity, ESD, and component traceability. Request process capability data for critical dimensions. The American Society for Quality reports that poor quality commonly costs 15–20% of sales. That figure makes prevention more valuable than final inspection. Look for documented CAPA ownership, measurable closure times, and recurring-failure analysis.
Testing should match product risk. AOI catches placement and solder defects. Automated X-ray reveals hidden voids and BGA connections. ICT checks electrical parameters, while functional testing confirms real operating behavior. Flying-probe testing suits lower-volume builds. Ask for sample reports, defect images, calibration records, and test coverage percentages. IPC industry survey findings continue to identify quality consistency and supply-chain control as major electronics manufacturing concerns. Do not accept vague claims. I would also inspect first-article records and microsection results when reliability matters. My own bias is simple: dashboards look impressive, but raw evidence tells the truth. Sometimes the supplier’s process is good, yet the test plan is incomplete. That deserves an honest review.
Comparing Costs, Lead Times, Communication, and Flexibility
Choosing a PCBA manufacturing partner requires more than comparing a quoted unit price. In practice, the lowest offer can become expensive after tooling changes, inspection fees, freight, and rework. Ask for a line-item estimate. Confirm whether testing, component sourcing, and engineering support are included. A reliable partner explains cost assumptions instead of hiding them behind one total. Small details matter. A five-day prototype promise may exclude material procurement.
Lead time should be measured from purchase order to tested shipment, not production start. Request a timeline covering sourcing, stencil preparation, assembly, inspection, and dispatch. Then test communication before signing. Send three practical questions and observe the response. Is it specific? Does an engineer join the discussion? Clear answers reduce delays when a component becomes unavailable. Weekly updates help, but a shared issue log is better. I have seen projects lose days because a minor footprint change waited for approval.
Flexibility becomes valuable when designs change. Check whether the factory supports small batches, revised bills of materials, and controlled substitutions without weakening traceability. Ask how urgent changes affect cost and schedule. A capable partner should explain limits honestly. No supplier gets everything right. Your team should also define approval rules, quality records, and escalation contacts. One overlooked weakness is communication across time zones; agree on response windows and backup contacts before the first build.
Selecting a Partner Through Samples, Audits, and Risk Assessment
Choosing a PCBA manufacturing partner requires more than comparing prices.
Start with samples that match your real design, not a convenient demonstration board. Inspect solder joints under magnification. Check component placement, connector alignment, and board cleanliness. Ask for test records, including AOI, in-circuit testing, and functional testing. A sample should reveal process discipline, not just visual polish.
Treat the factory audit as evidence gathering.
Review incoming inspection, humidity control, ESD protection, and material traceability. Walk through the production line and observe how operators handle rejected boards. Ask to see calibration records and recent corrective-action reports. Experienced teams can explain failure patterns clearly. Vague answers deserve attention. An audit snapshot is never complete.
Risk assessment should connect technical details with business consequences.
Examine approved supplier controls, component availability, backup equipment, production capacity, and engineering response times. Request a pilot build before committing to volume. Track defects by type, repair hours, and delivery performance. One overlooked connector can delay an entire shipment. I have seen clean samples hide weak documentation. That possibility should shape the review. No partner is risk-free, and no checklist replaces informed judgment.