How to Choose the Right PCBA Manufacturing Partner
Choosing the right pcba manufacturing partner is a decision about more than unit price. It affects product quality, delivery reliability, and how quickly design problems surface. Grand View Research estimated the global printed circuit board market at $73.4 billion in 2023. That figure describes the PCB market, not PCBA services, but it signals the scale and complexity of the supply chain. Shigeo Shingo, a manufacturing engineer whose work influenced modern production systems, cautioned, “The most dangerous kind of waste is the waste we do not recognize.” Hidden waste can appear as repeated defects, unclear change control, or idle time between process steps. Small details matter.
A useful partner should explain its process with evidence. Ask how it handles design-for-manufacturing reviews, component traceability, inspection, and corrective action. Request examples of inspection records and production reports, not just a polished capability sheet. Check whether its equipment and staff can support your board’s layer count, package types, volumes, and testing needs. IPC standards such as IPC-A-610 and J-STD-001 can help frame quality discussions; they do not replace a review of the supplier’s actual controls. Visit the production floor if practical. Watch how materials are labeled, stored, and tracked. Then compare realistic lead times, communication practices, and escalation paths. A low quote may still be the wrong fit. I would also question any supplier that promises zero defects without explaining its measurement method. No checklist removes every risk. The goal is a partner that identifies problems early, shares credible data, and improves with your team.
Define Your PCBA Project Requirements and Quality Standards
Before comparing PCBA manufacturing partners, define the project in measurable terms. Record the board dimensions, layer count, material, copper weight, and expected annual volume. Include the complete bill of materials, approved alternatives, and component lifecycle risks. State critical features, such as controlled impedance, fine-pitch packages, or thermal requirements. Add assembly tolerances and the required testing method. These details give suppliers a practical basis for quoting and process planning. Small gaps matter.
Your quality standard should describe acceptance criteria, not simply request “high quality.” Specify inspection points, solder joint requirements, cleanliness limits, and electrical test coverage. Ask for documented traceability from incoming materials to finished boards. A capable partner should explain its process controls, calibration records, and corrective-action workflow. In production reviews, I have found that sample approval can hide repeatability problems. Request pilot builds, first-article reports, and measurable yield data before scaling. Also discuss how deviations will be reported and approved. No process is perfect. Your requirements may need revision after the first build, especially when test fixtures reveal access problems or assembly tolerances prove unrealistic. Clear records and honest technical discussions make those changes safer.
How to Choose the Right PCBA Manufacturing Partner
Define Your PCBA Project Requirements and Quality Standards
This illustrative planning index prioritizes the evidence a PCBA manufacturer should provide before supplier selection. Quality standards, test coverage, traceability, design-for-manufacturing capability, supply continuity, and documentation should be defined and verified against the product's risk level and applicable IPC requirements.
Evaluate Manufacturing Capabilities, Technology, and Production Capacity
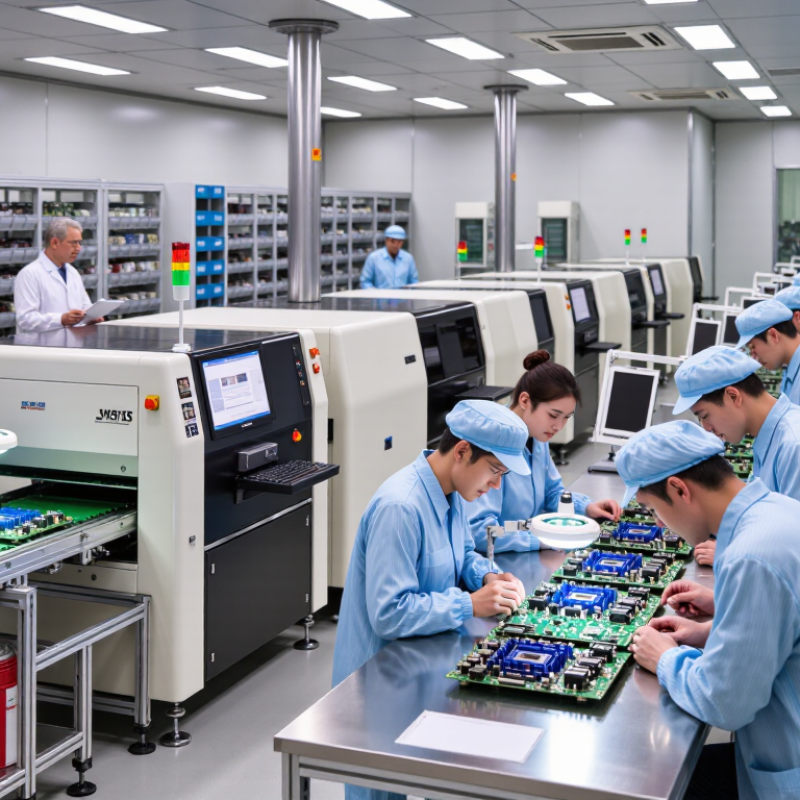
Choosing a PCBA manufacturing partner requires evidence, not attractive brochures. Ask for recent examples involving similar board layers, component density, tolerances, and compliance requirements. Review the factory’s SMT line count, placement accuracy, solder-paste inspection, automated optical inspection, and X-ray coverage. Technology must match the board’s actual risks.
Capacity needs careful measurement. Request monthly placement capacity, line utilization, changeover time, and available shifts. A large number can mislead when utilization already exceeds 85%. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. This signals stronger automation, but robots alone cannot prove process control. Check calibration records, first-pass yield, defect-per-million data, and corrective-action reports. Ask how the factory handles a missing component reel at 2 a.m.
Production planning also reveals maturity. Compare quoted lead times with historical delivery performance across at least six months. The IPC Electronics Industry Sentiment Survey regularly tracks pressure from material costs, demand changes, and labor shortages. These pressures can expose weak capacity planning. A capable partner should show dual-source strategies, traceability from reel to finished board, and documented engineering-change control.
Do not trust every dashboard. A weakness in my own supplier audits has been accepting averages without examining failed lots. Request anonymized production records and observe a live line, if possible. Confirm whether testing includes in-circuit testing, functional testing, or boundary-scan coverage. The best evaluation connects equipment, people, data, and realistic output—not impressive machinery sitting quietly.
Verify Certifications, Quality Systems, and Supply Chain Control
An attractive quotation means little if a factory cannot prove control.
Request copies of current certificates, their scope, and expiration dates. Verify that the listed site matches the facility building your boards. Relevant standards may include ISO 9001 or sector-specific quality requirements. Do not accept a certificate alone. Ask how audits are handled and whether findings receive documented corrective action.
During a factory review, examine training records, calibration labels, and controlled work instructions. Look for traceability from incoming components to finished assemblies. Sample records should show solder-paste inspection, automated optical inspection, testing, and rework history. Photos are useful, but original records are stronger evidence. Ask to see a redacted report, not just a polished presentation. Small gaps often reveal more than impressive equipment.
Supply chain control deserves equal attention.
Request an approved-vendor process, component authentication steps, and rules for substitutions. Your partner should identify risks before a shortage reaches production. Check whether critical parts have qualified alternatives, realistic safety stock, and documented change notification. Traceability should include lot numbers, date codes, and purchase records. In one review, a missing date-code check exposed a risk that paperwork had hidden. That mistake was fixable, but it changed our supplier evaluation. Ask who owns escalation, how quickly you receive alerts, and what evidence supports recovery plans. Promises are not controls. Verify them on the factory floor.
Compare Costs, Communication, Lead Times, and Customer Support
A PCBA quote should show more than the board’s unit price. Compare setup fees, stencil costs, inspection, packaging, and shipping on the same production quantity. Ask what happens if the design changes after the quote. A low number can hide extra charges. Check the assumptions.
Communication is part of manufacturing quality. Ask who will answer engineering questions and how quickly you can expect a response. Share a sample issue, such as a missing component value, and notice whether the reply is clear and specific. I find this easy to underestimate: a spreadsheet may compare prices, but it cannot show how much time unclear ownership will cost. No partner is perfect. The important thing is how problems are reported and resolved.
Lead times need careful checking. Request a schedule that separates material sourcing, assembly, inspection, and shipping. Confirm which dates depend on component availability, and ask how delays are communicated. A short promise is not useful if it leaves no room for a backordered part. Customer support matters after delivery, too. Ask how defects are documented, whether production records can be traced to a lot, and what information is needed to investigate a board that fails testing. Clear answers make comparisons more reliable.
Assess Samples, Risk Management, and Long-Term Partnership Potential
How to Choose the Right PCBA Manufacturing Partner
Assess Samples, Risk Management, and Long-Term Partnership Potential
Choosing a PCBA manufacturing partner starts with evidence, not persuasive presentations. Request production samples matching your board’s layer count, component density, and finishing requirements. Inspect solder joints under magnification. Look for voids, lifted pads, uneven coating, and inconsistent connector alignment. Ask for traceability records, inspection images, and test results linked to each sample. A beautiful prototype proves little. Still, it reveals process discipline. Evaluate whether the supplier explains defects openly instead of hiding behind perfect photographs.
Risk management should be specific and measurable. Review component verification, approved alternates, storage controls, and counterfeit prevention procedures. Ask how the supplier handles shortages, engineering changes, and sudden test failures. A useful response includes owners, deadlines, escalation paths, and corrective actions. Check continuity plans for equipment breakdowns, power interruptions, and workforce shortages. Do not accept vague promises. Request a small pilot run before full-volume production. Track first-pass yield, rework rate, delivery accuracy, and response time. Numbers expose uncomfortable gaps. Some gaps are fixable.
Long-term partnership depends on communication as much as capacity. Assess whether engineers ask precise questions about tolerances, test access, thermal limits, and assembly risks. Reliable partners challenge unclear drawings respectfully. They also protect revisions through controlled document systems. Review how pricing changes when volumes, materials, or schedules shift. A low initial quote may become expensive after repeated rework. I have seen teams overvalue speed and undervalue reporting. That judgment can fail. Choose a partner willing to share bad news early and improve through measurable actions. Trust grows through repeated deliveries, honest reviews, and fewer surprises.